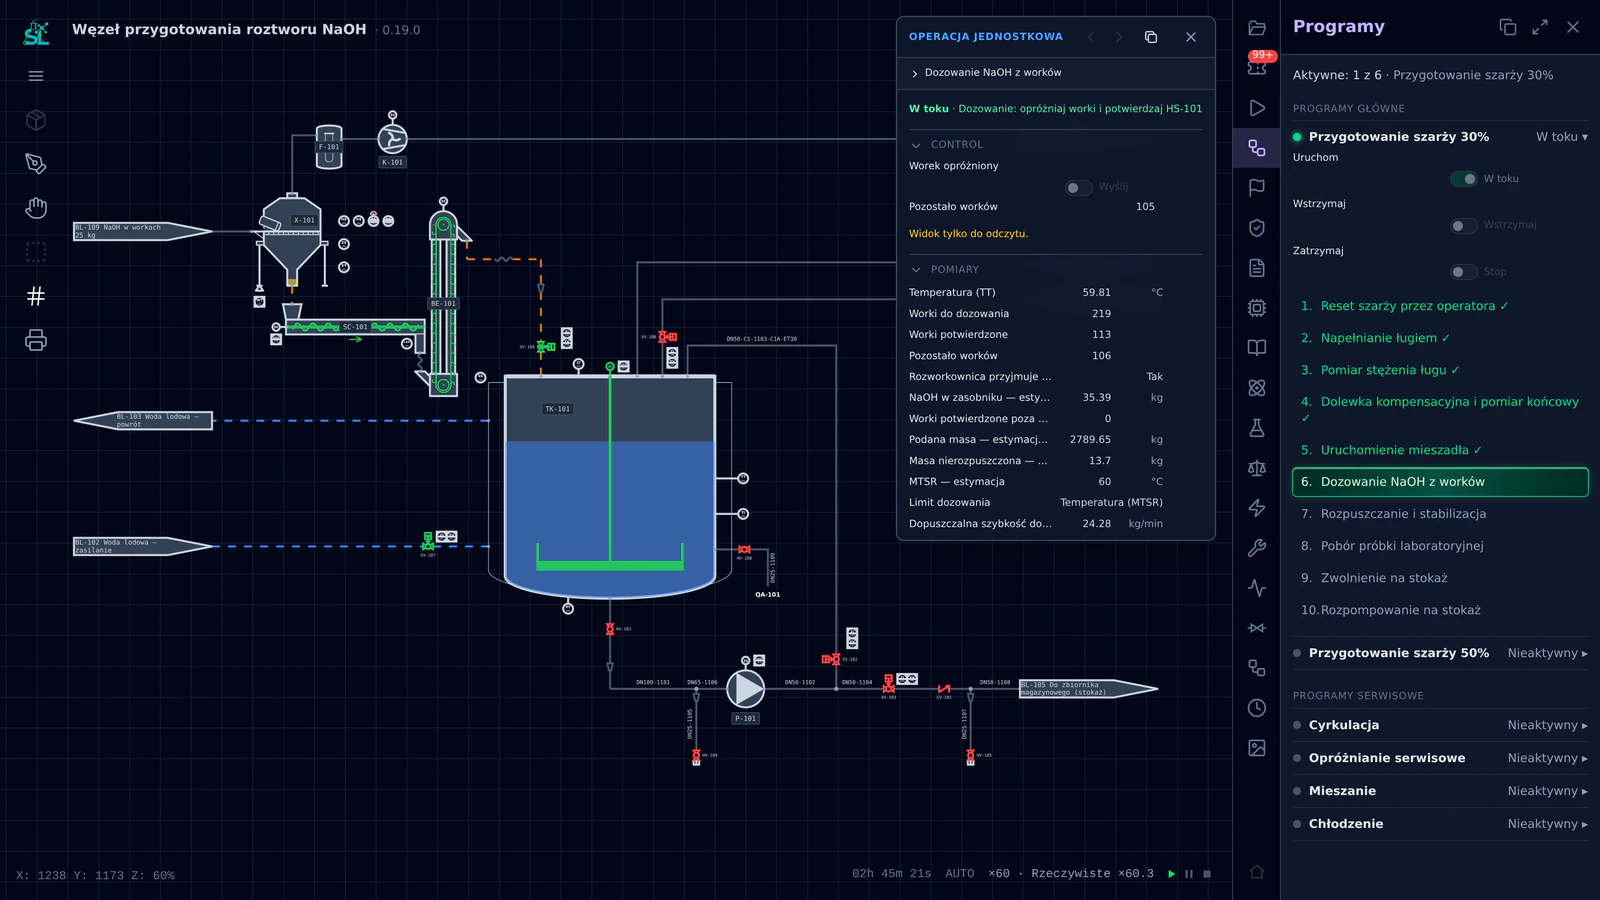
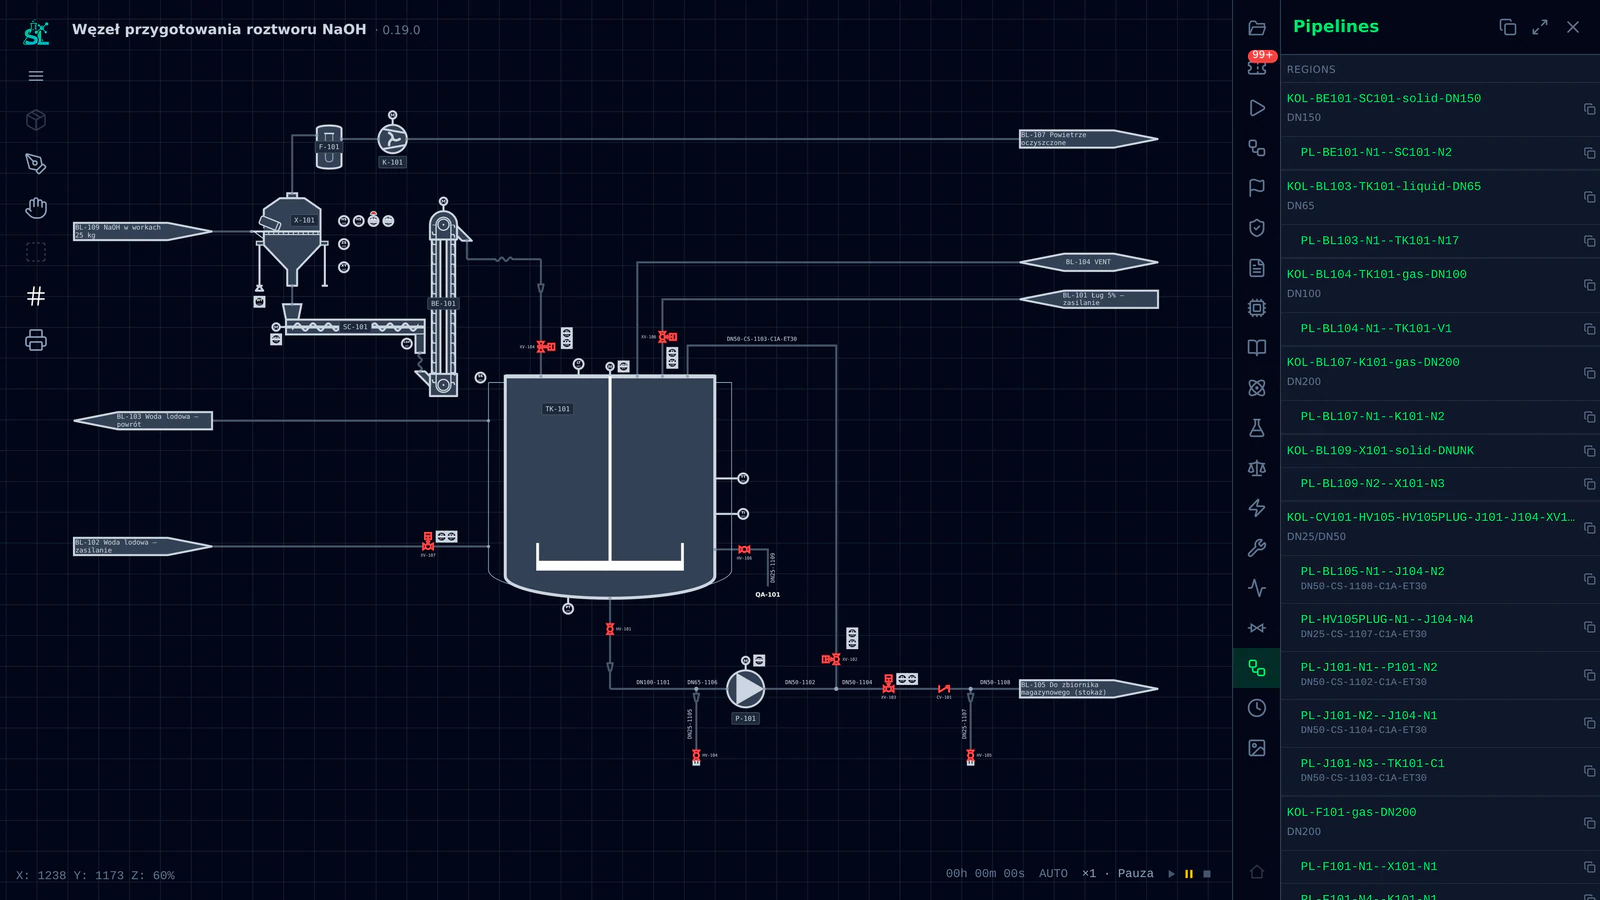
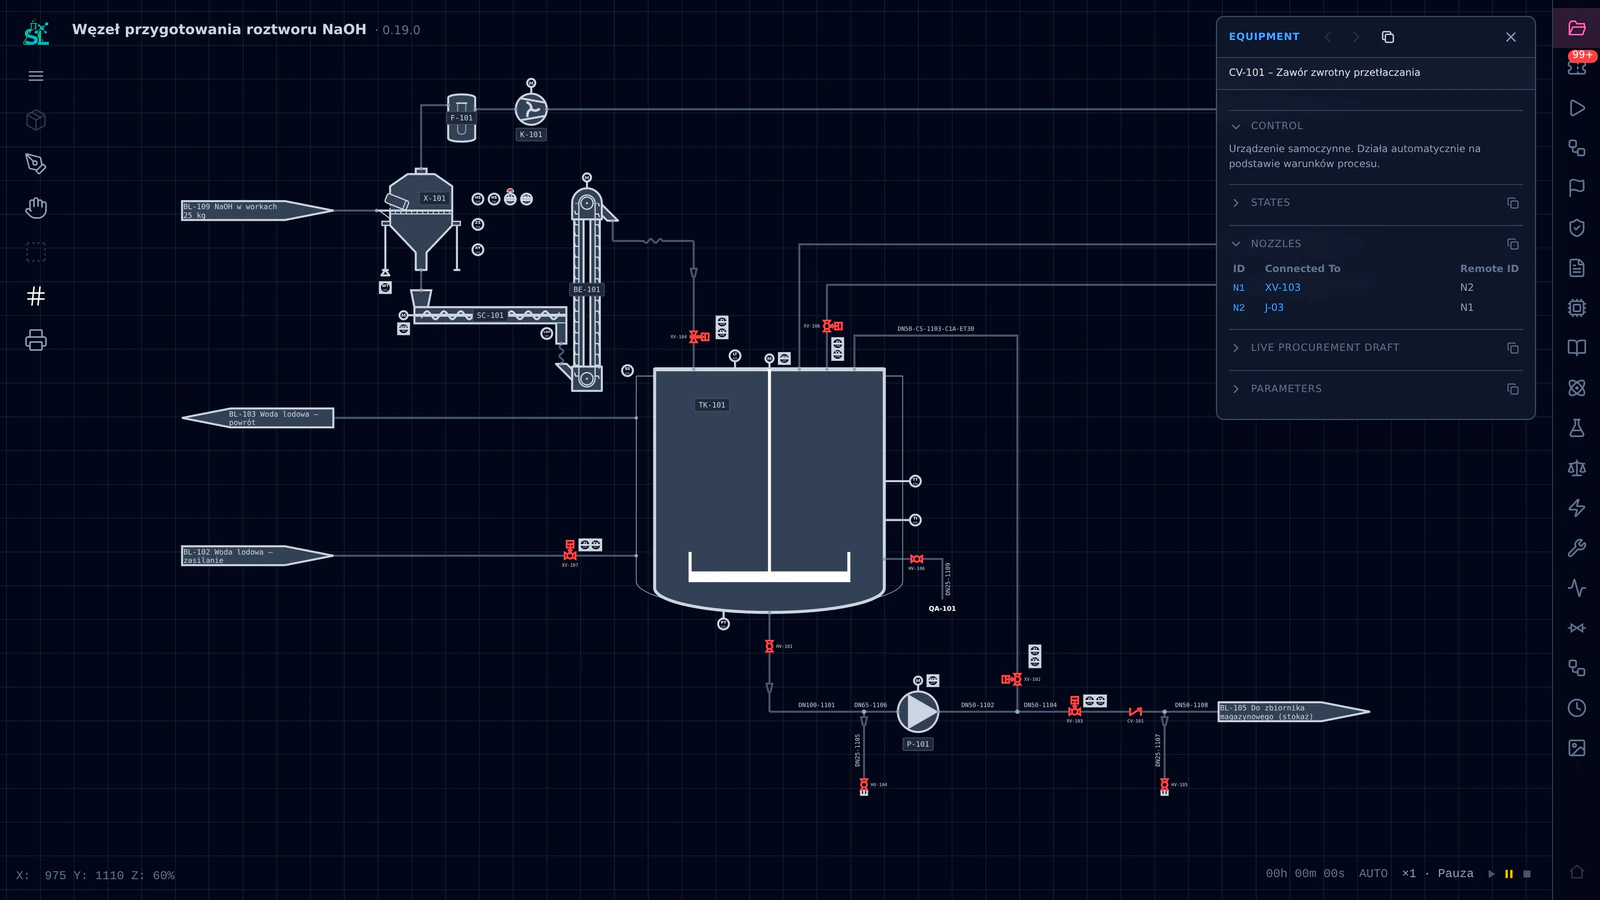
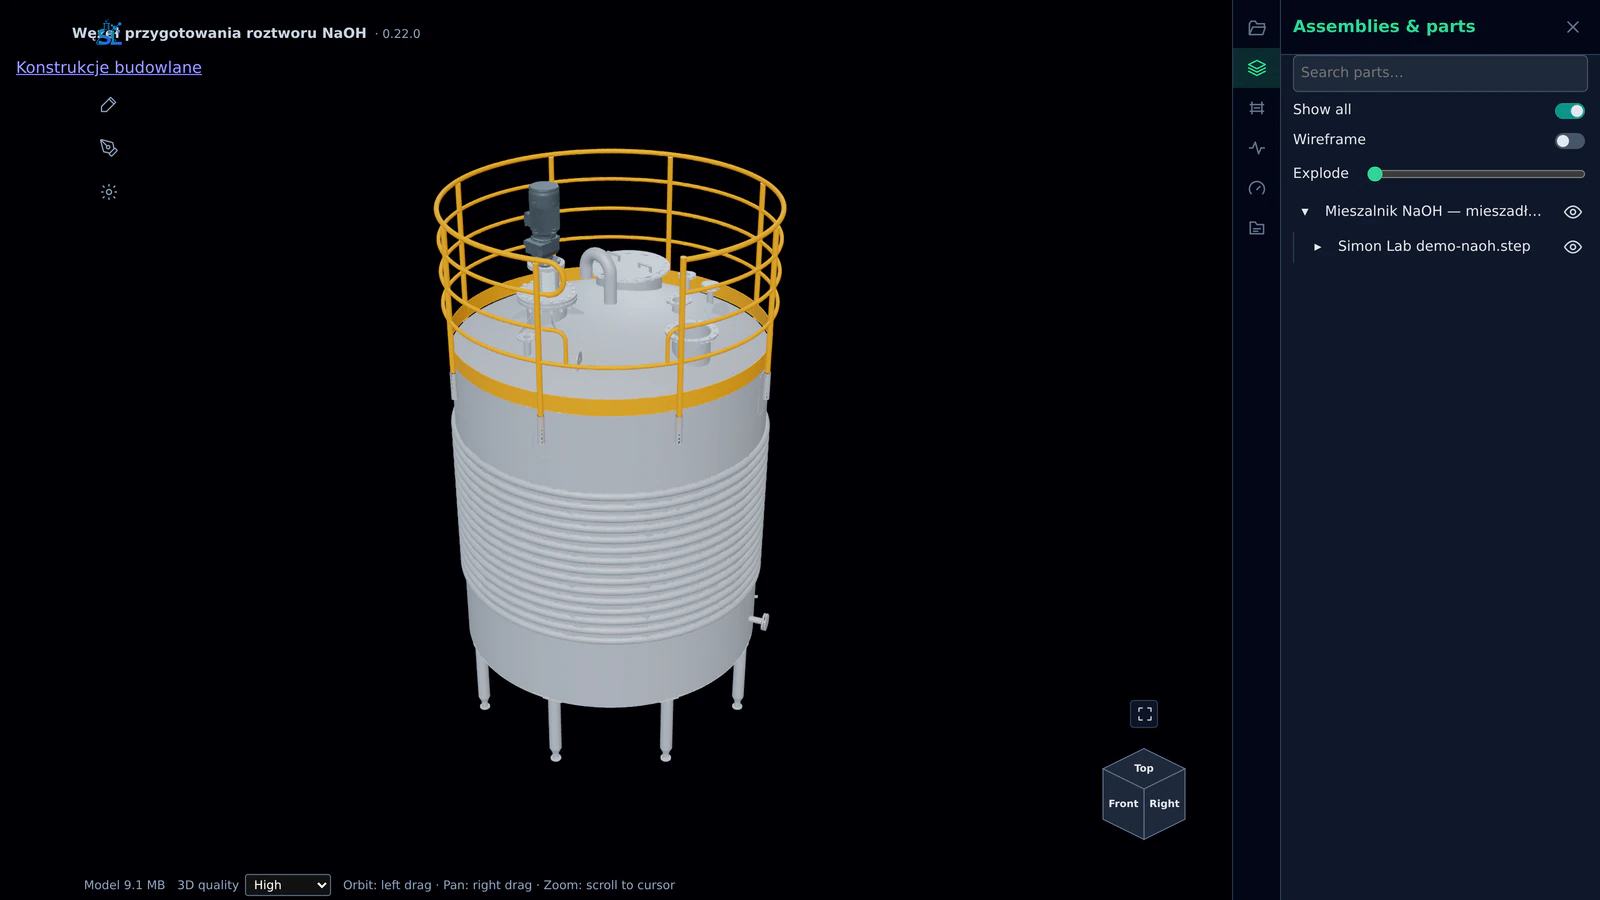
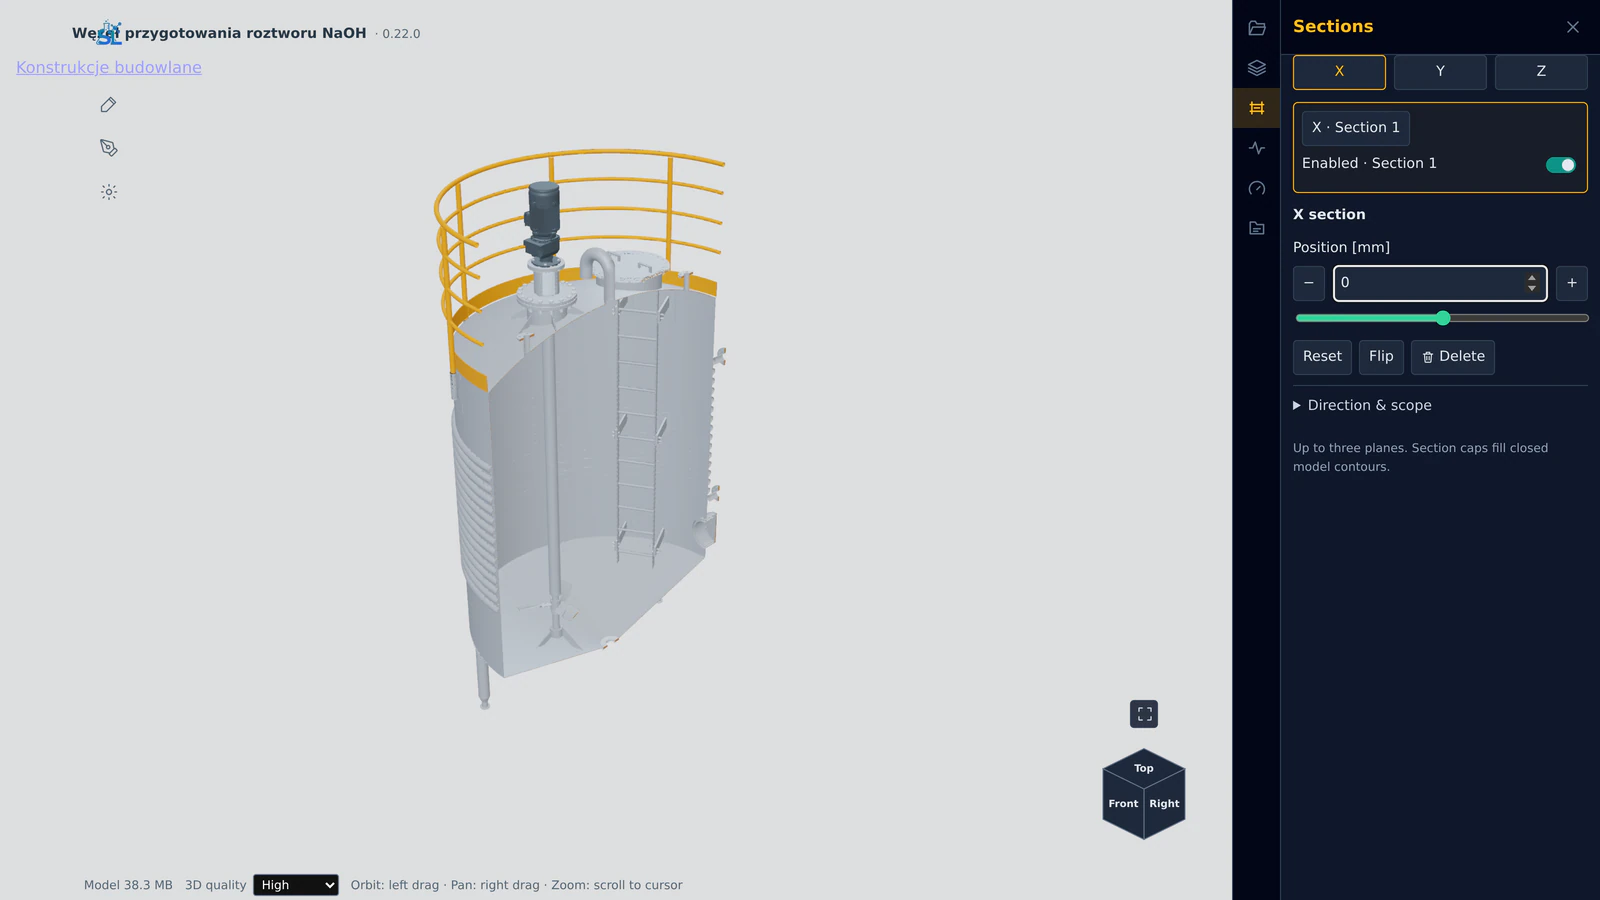
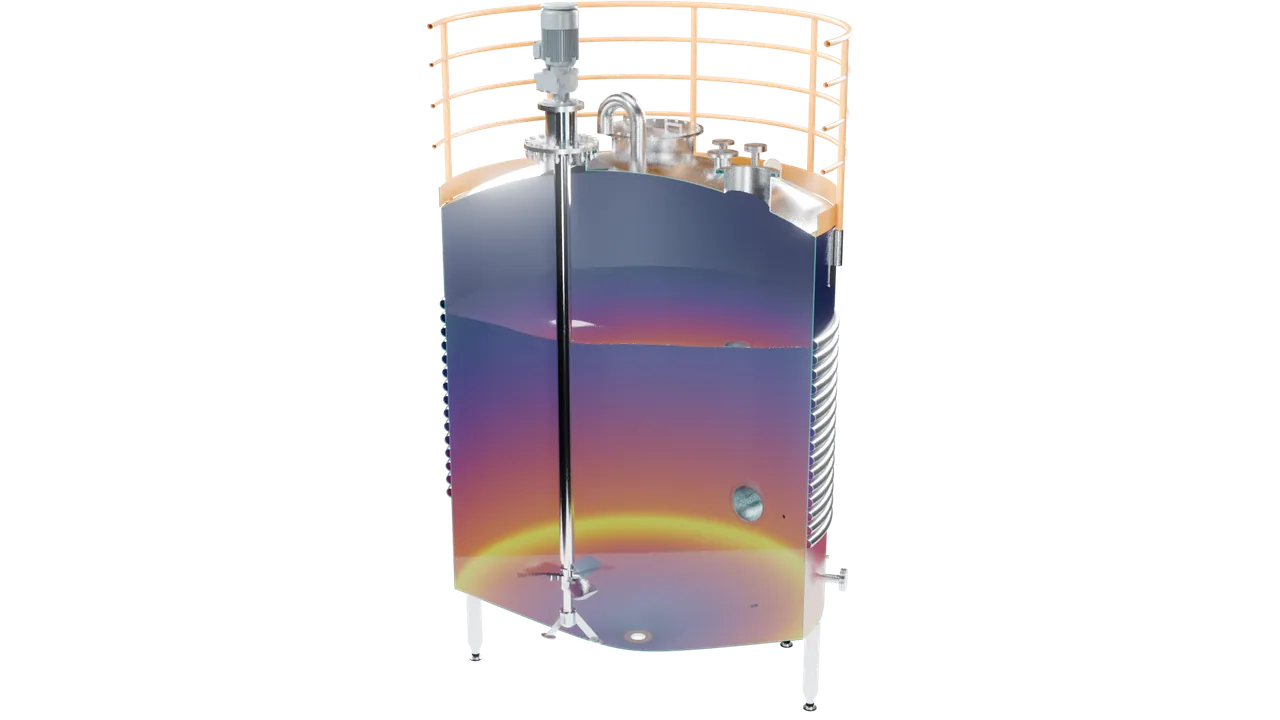
› Bring 5% lye to 30% with NaOH flakes from 25 kg bags, 14.5 m³ batch, max 60 °C in the tank, 40 °C at discharge. Design it with a bottom-up approach, layer by layer, and fit it into a spare area of my plant.
describe a process, a unit or a change… ✦ reading NaOH–H₂O thermodynamics…
✦ balancing mass and heat of dissolution…
✦ sizing agitation and cooling duty…
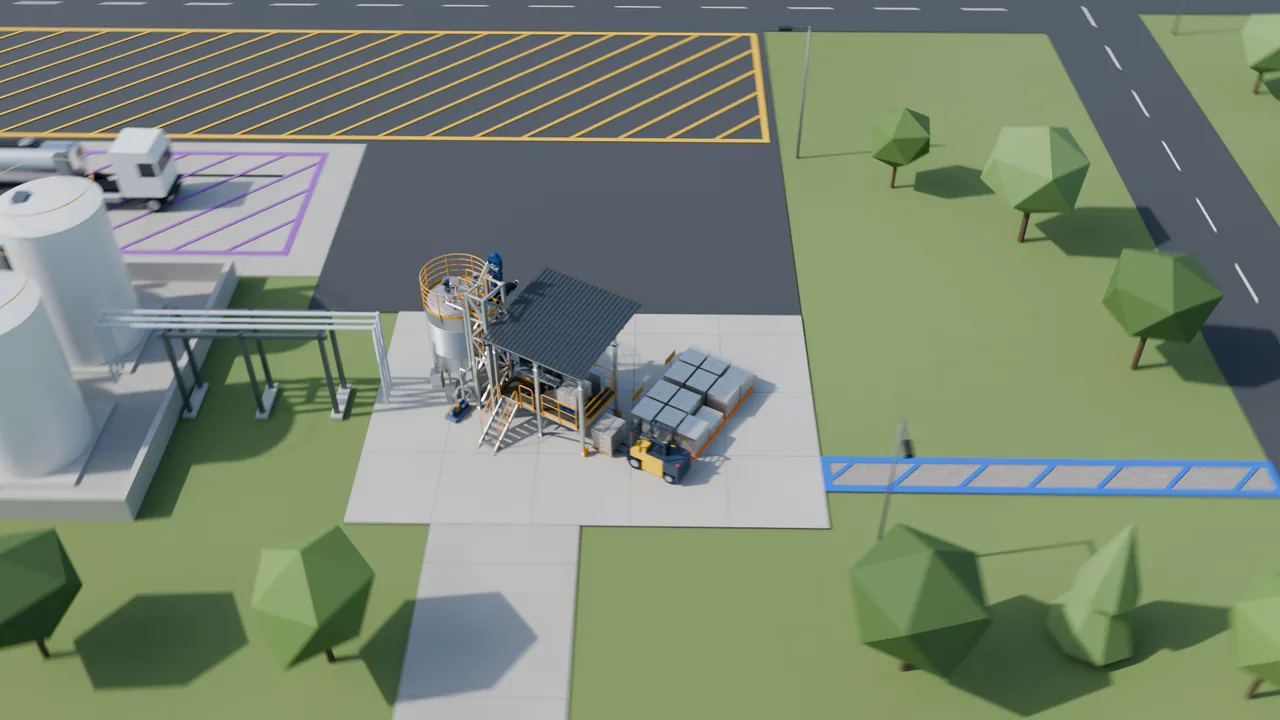
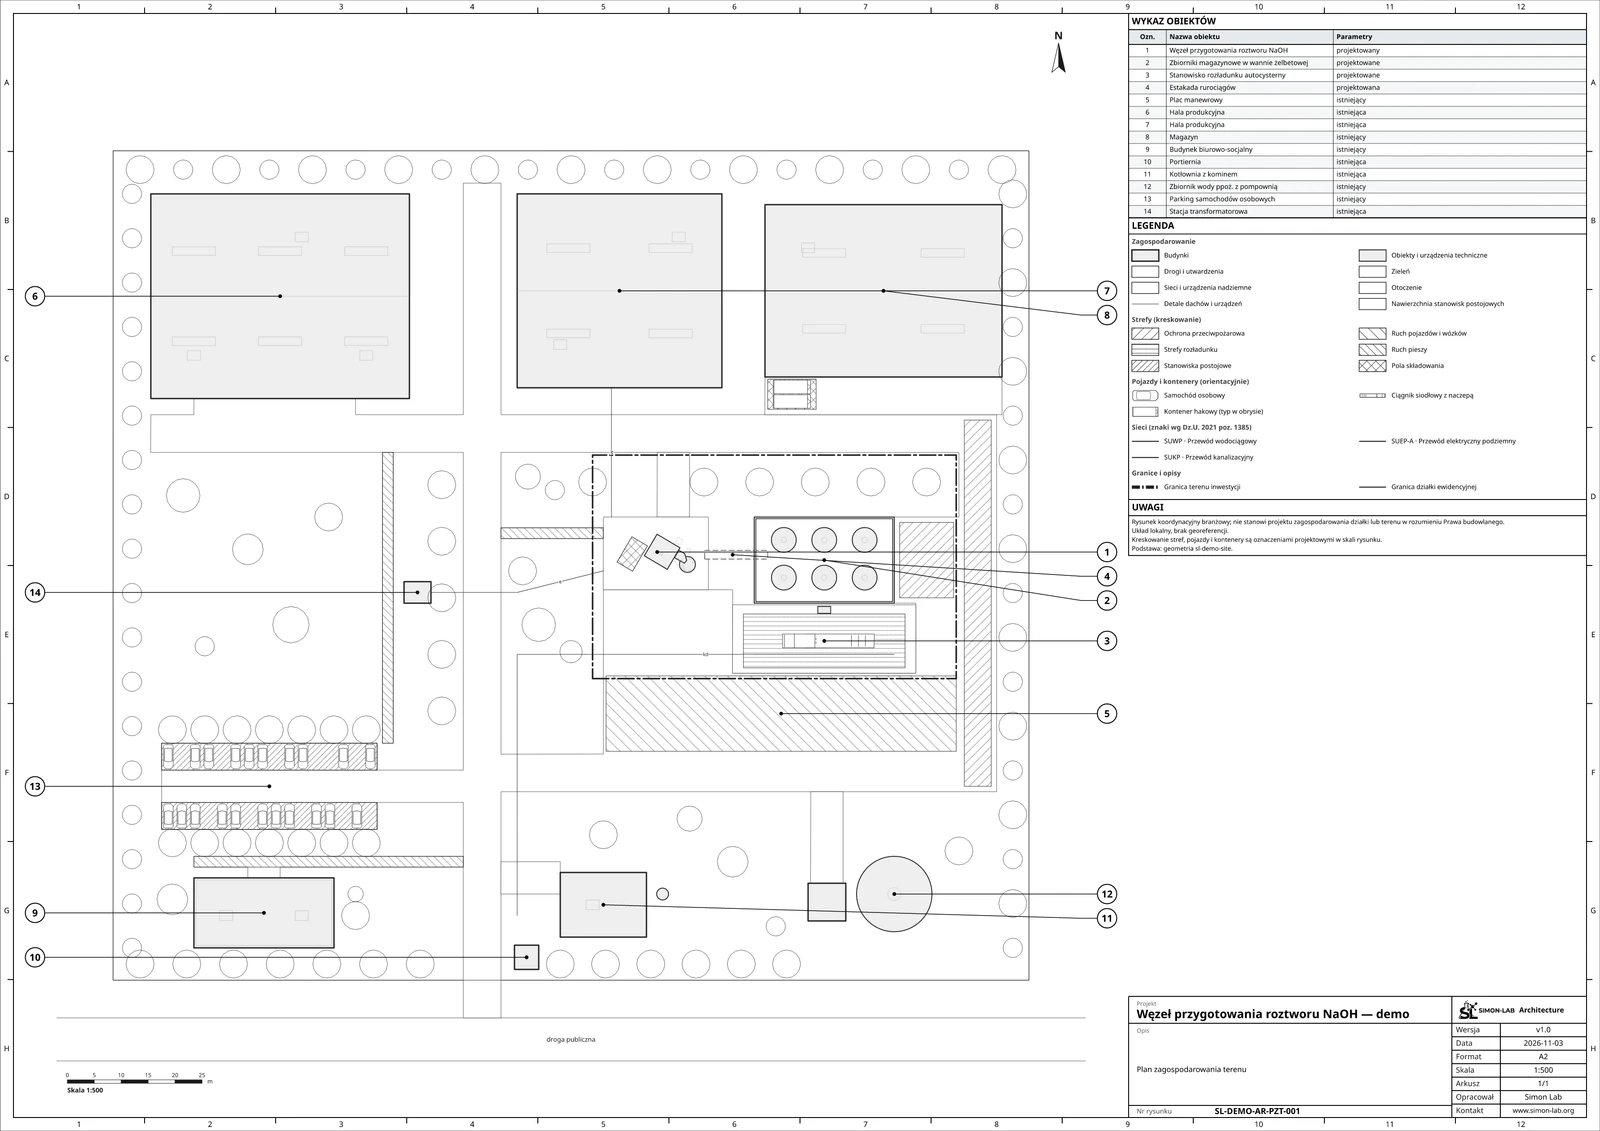
✦ scanning the site for a spare plot…
✦ drafting the design basis…
● SPEC · NaOH dissolving unit · draft 1
DESIGN BASIS
product 30 % w/w NaOH · 14.5 m³ per batch
feed 5 % lye + NaOH flakes · 220 × 25 kg bags = 5.5 t per batch
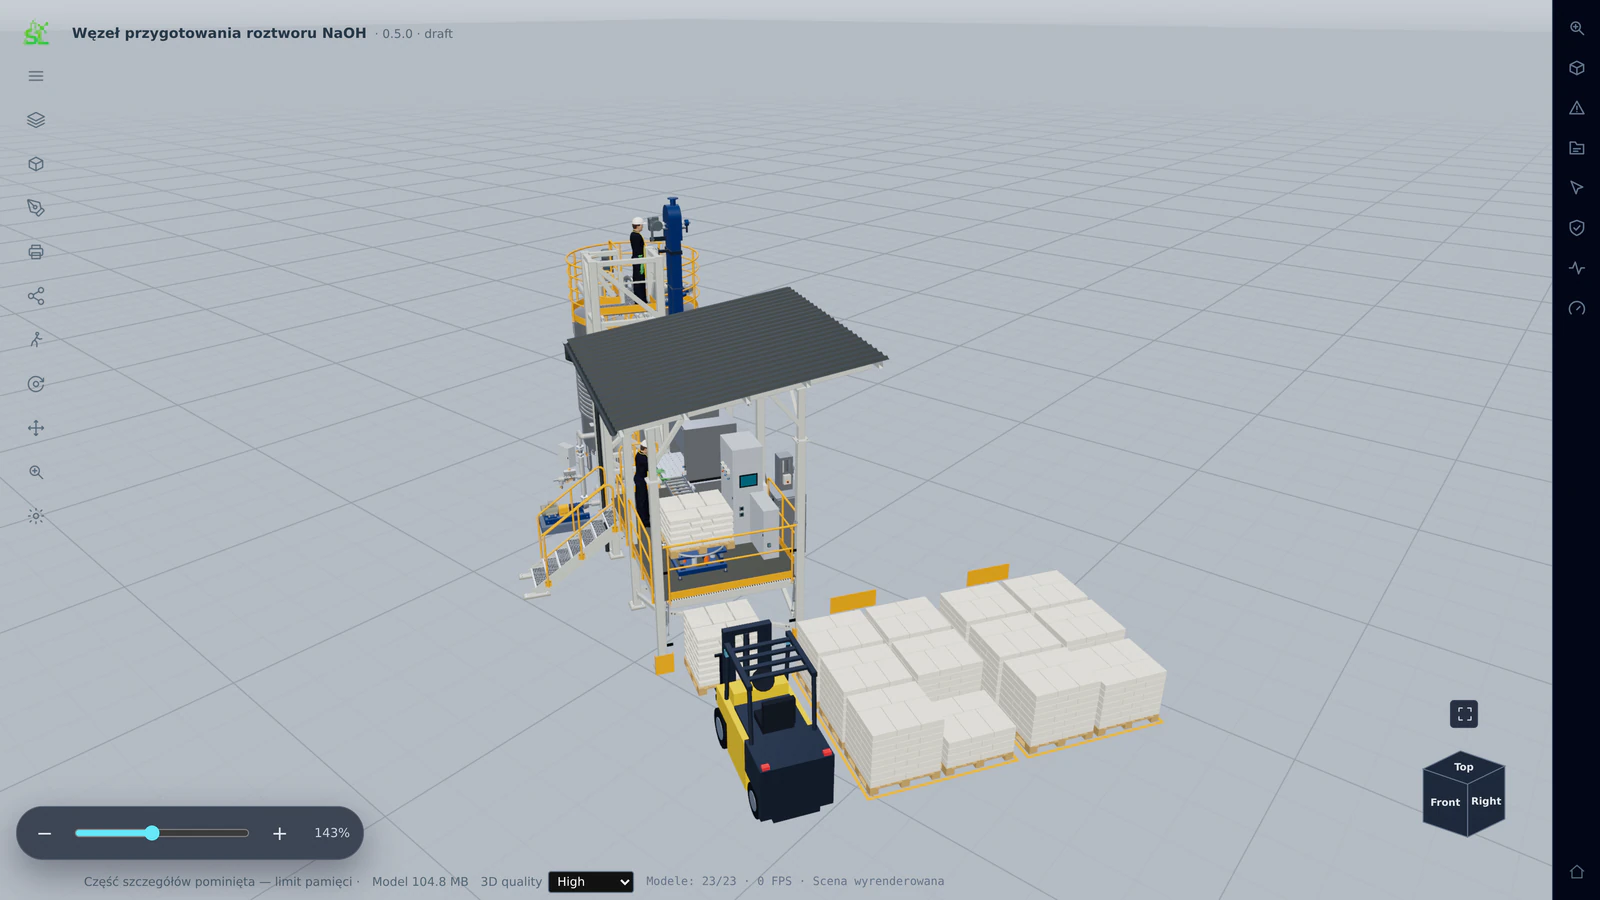
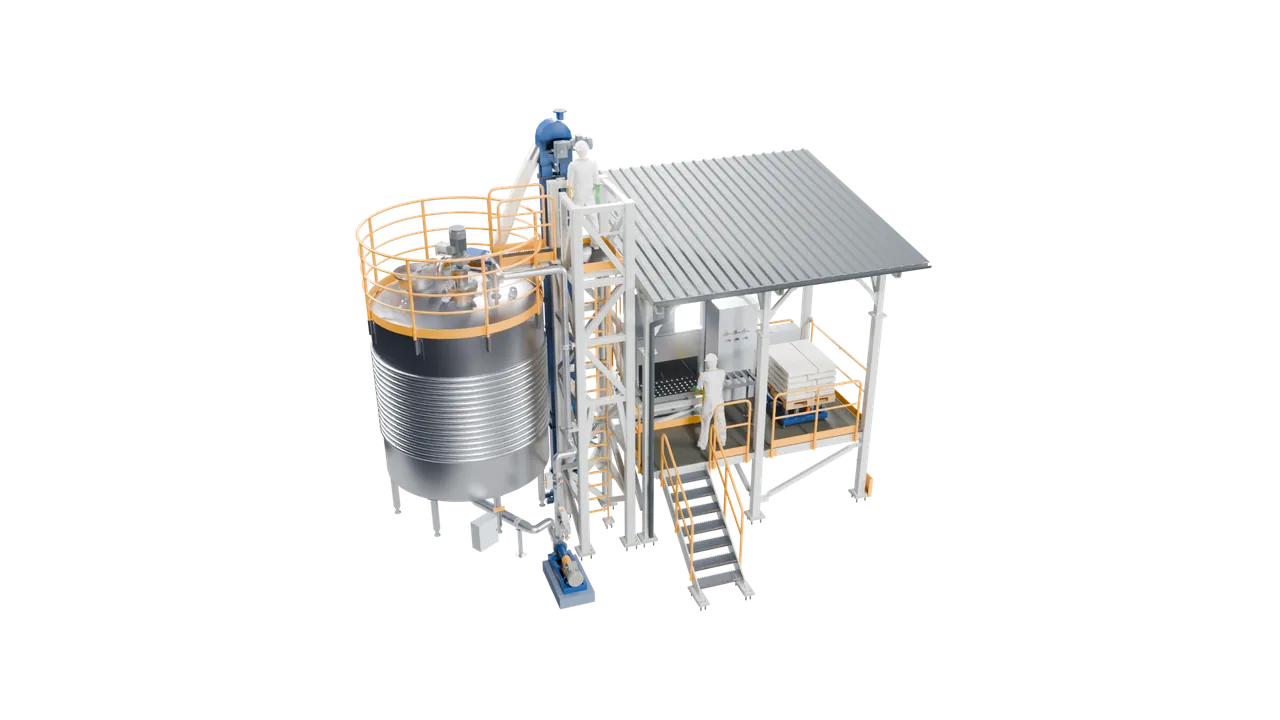
handling bag-dump station · 2 bags/min · 25 kg within manual-handling limits
limits ≤ 60 °C in the tank · 40 °C at discharge
utilities chilled water 7.5 °C · half-pipe cooling jacket
vessel existing stainless tank · retrofit
PHYSICS FIRST
▸ dissolution is exothermic → dosing rate bounded by cooling duty
▸ density and viscosity 5 → 30 % from NaOH–H₂O property models
▸ solids suspension and power number → agitator selection
CAPACITY & ECONOMICS
▸ demand ≥ 60 m³ of lye per week · 3 shifts × 8 h · 7 days
▸ lye fill and pump-out 10 m³/h each → one batch fits one shift
▸ retrofit of the existing tank instead of a new vessel
LAYERS · bottom-up
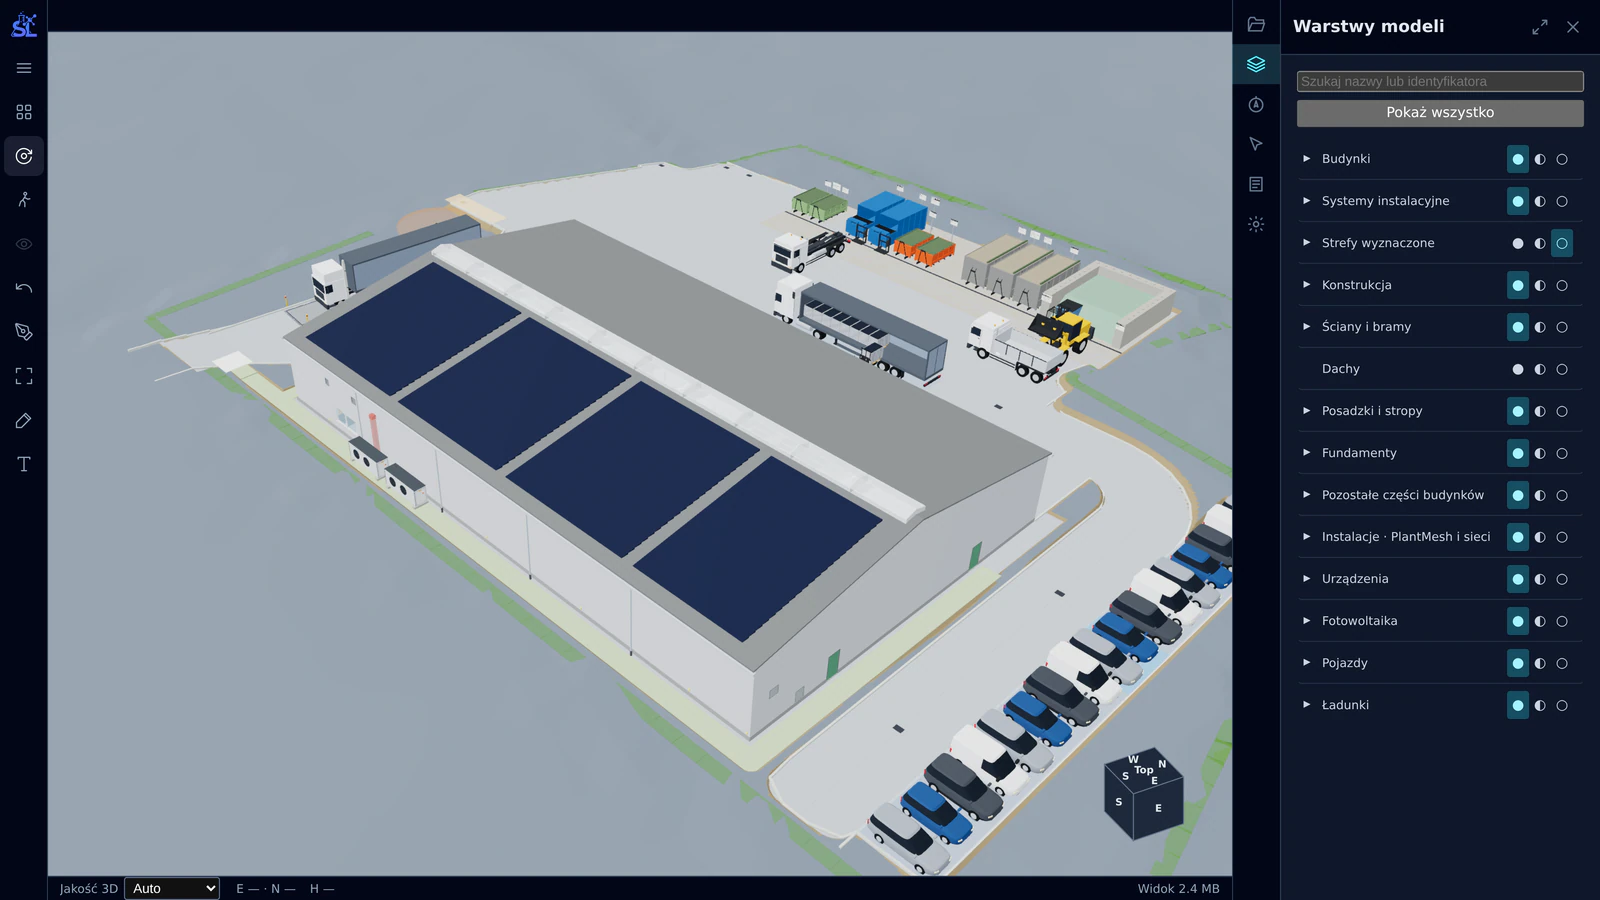
4 Architecture spare area on site · roads · site plan
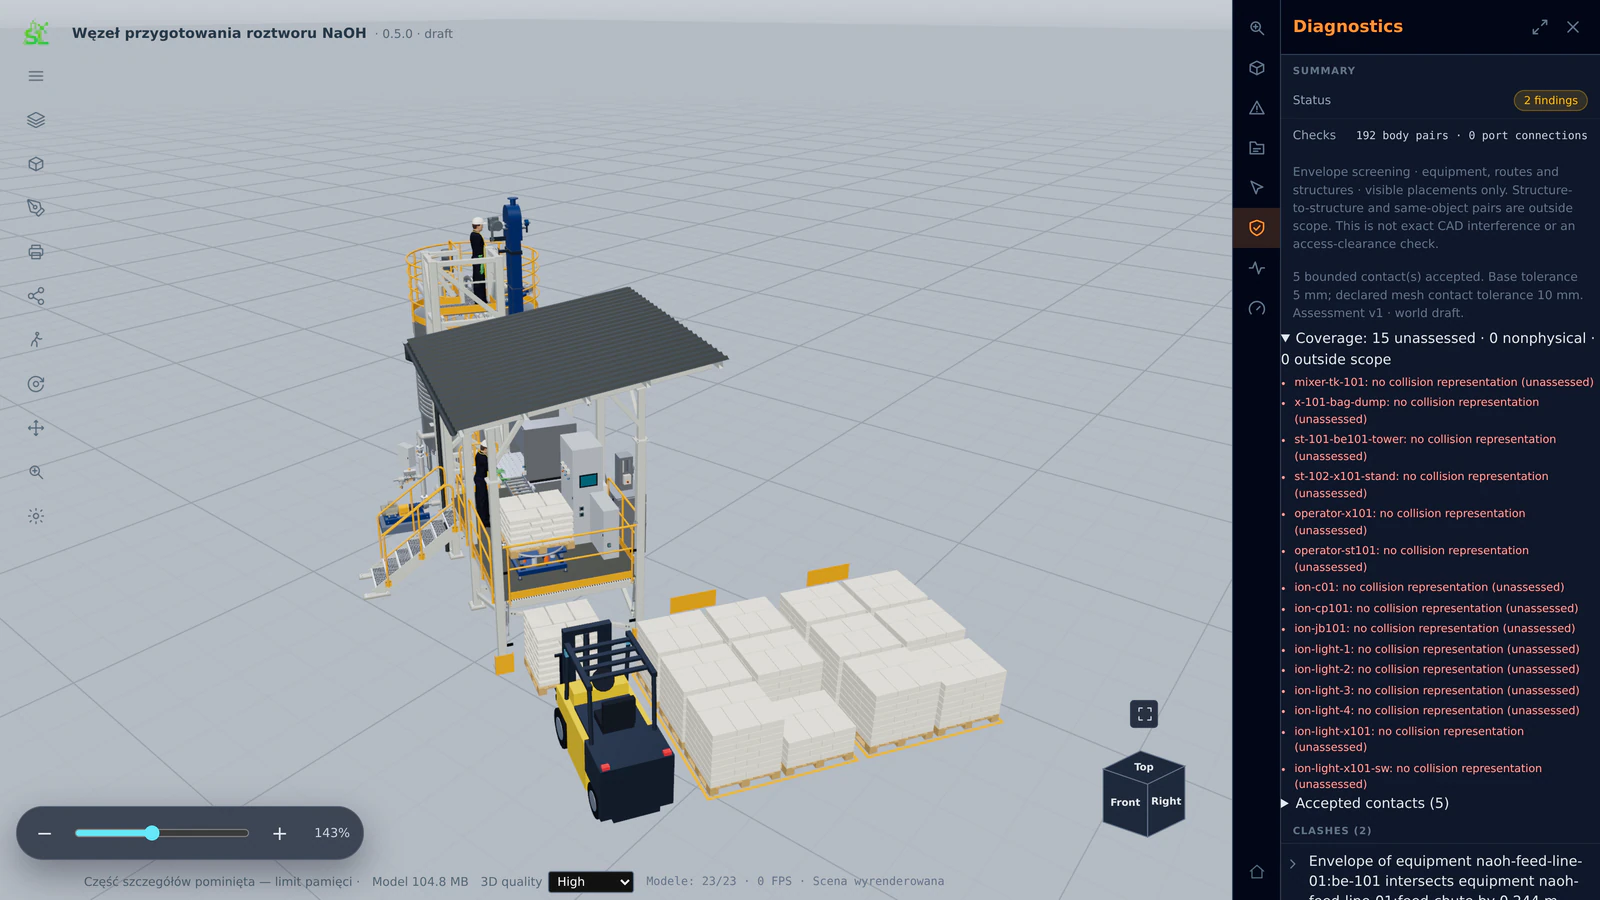
3 PlantMesh 3D assembly · isometrics · supports · clashes
2 MechGraph vessel · agitator · shaft · CFD
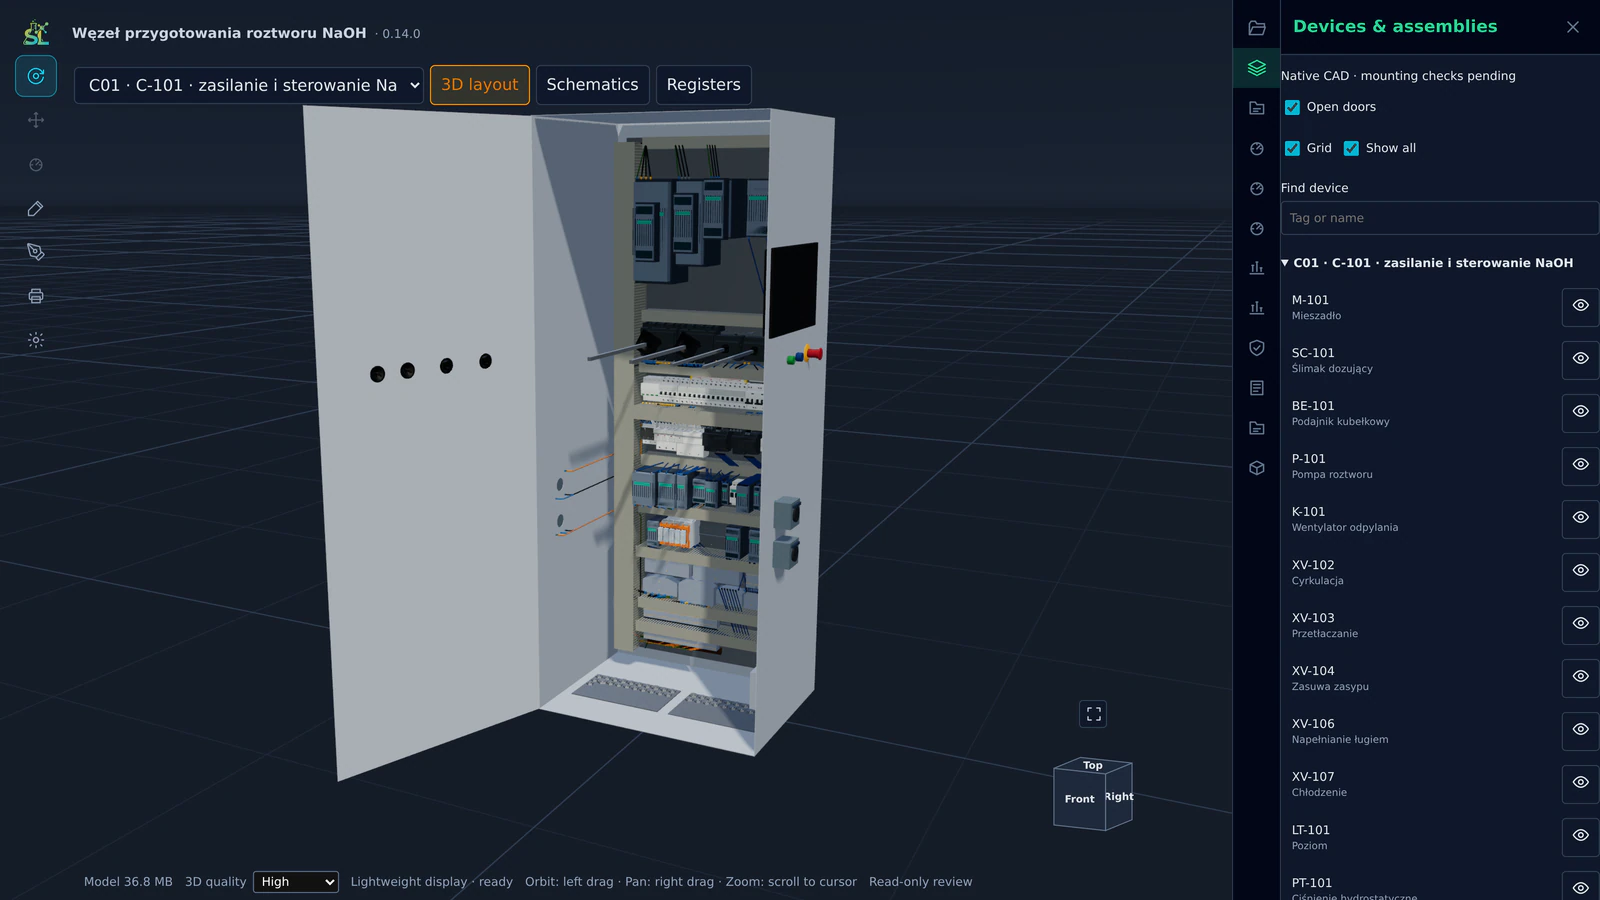
IonGrid control cabinets · I/O · heat gains
1 ProcessView P&ID · selections · dynamic simulation
0 CapacityIndex scope · capacity · economics ● this spec
OPEN POINTS
▸ flake purity and size distribution: confirm with the supplier
▸ dust extraction and empty-bag handling at the station